
A Practical Supplier Qualification Checklist for Pharmaceutical Procurement
Use this practical, risk based supplier qualification checklist to assess pharma suppliers, document control expectations, and reduce delivery and quality risk.
Pharmaceutical procurement cannot treat supplier qualification as a box ticking form. In regulated manufacturing, a supplier can look commercially attractive and still be the wrong choice because its quality system, documentation discipline, or change control behaviour is weak. That is why a serious qualification process has to be risk based, driven by evidence, and shared across functions.[1, 2]
Why this matters now
The regulatory baseline is clear. The pharmaceutical company remains ultimately responsible for outsourced activities and the quality of purchased materials. That means procurement cannot separate price from quality oversight and say the rest belongs to QA later.[1, 3]
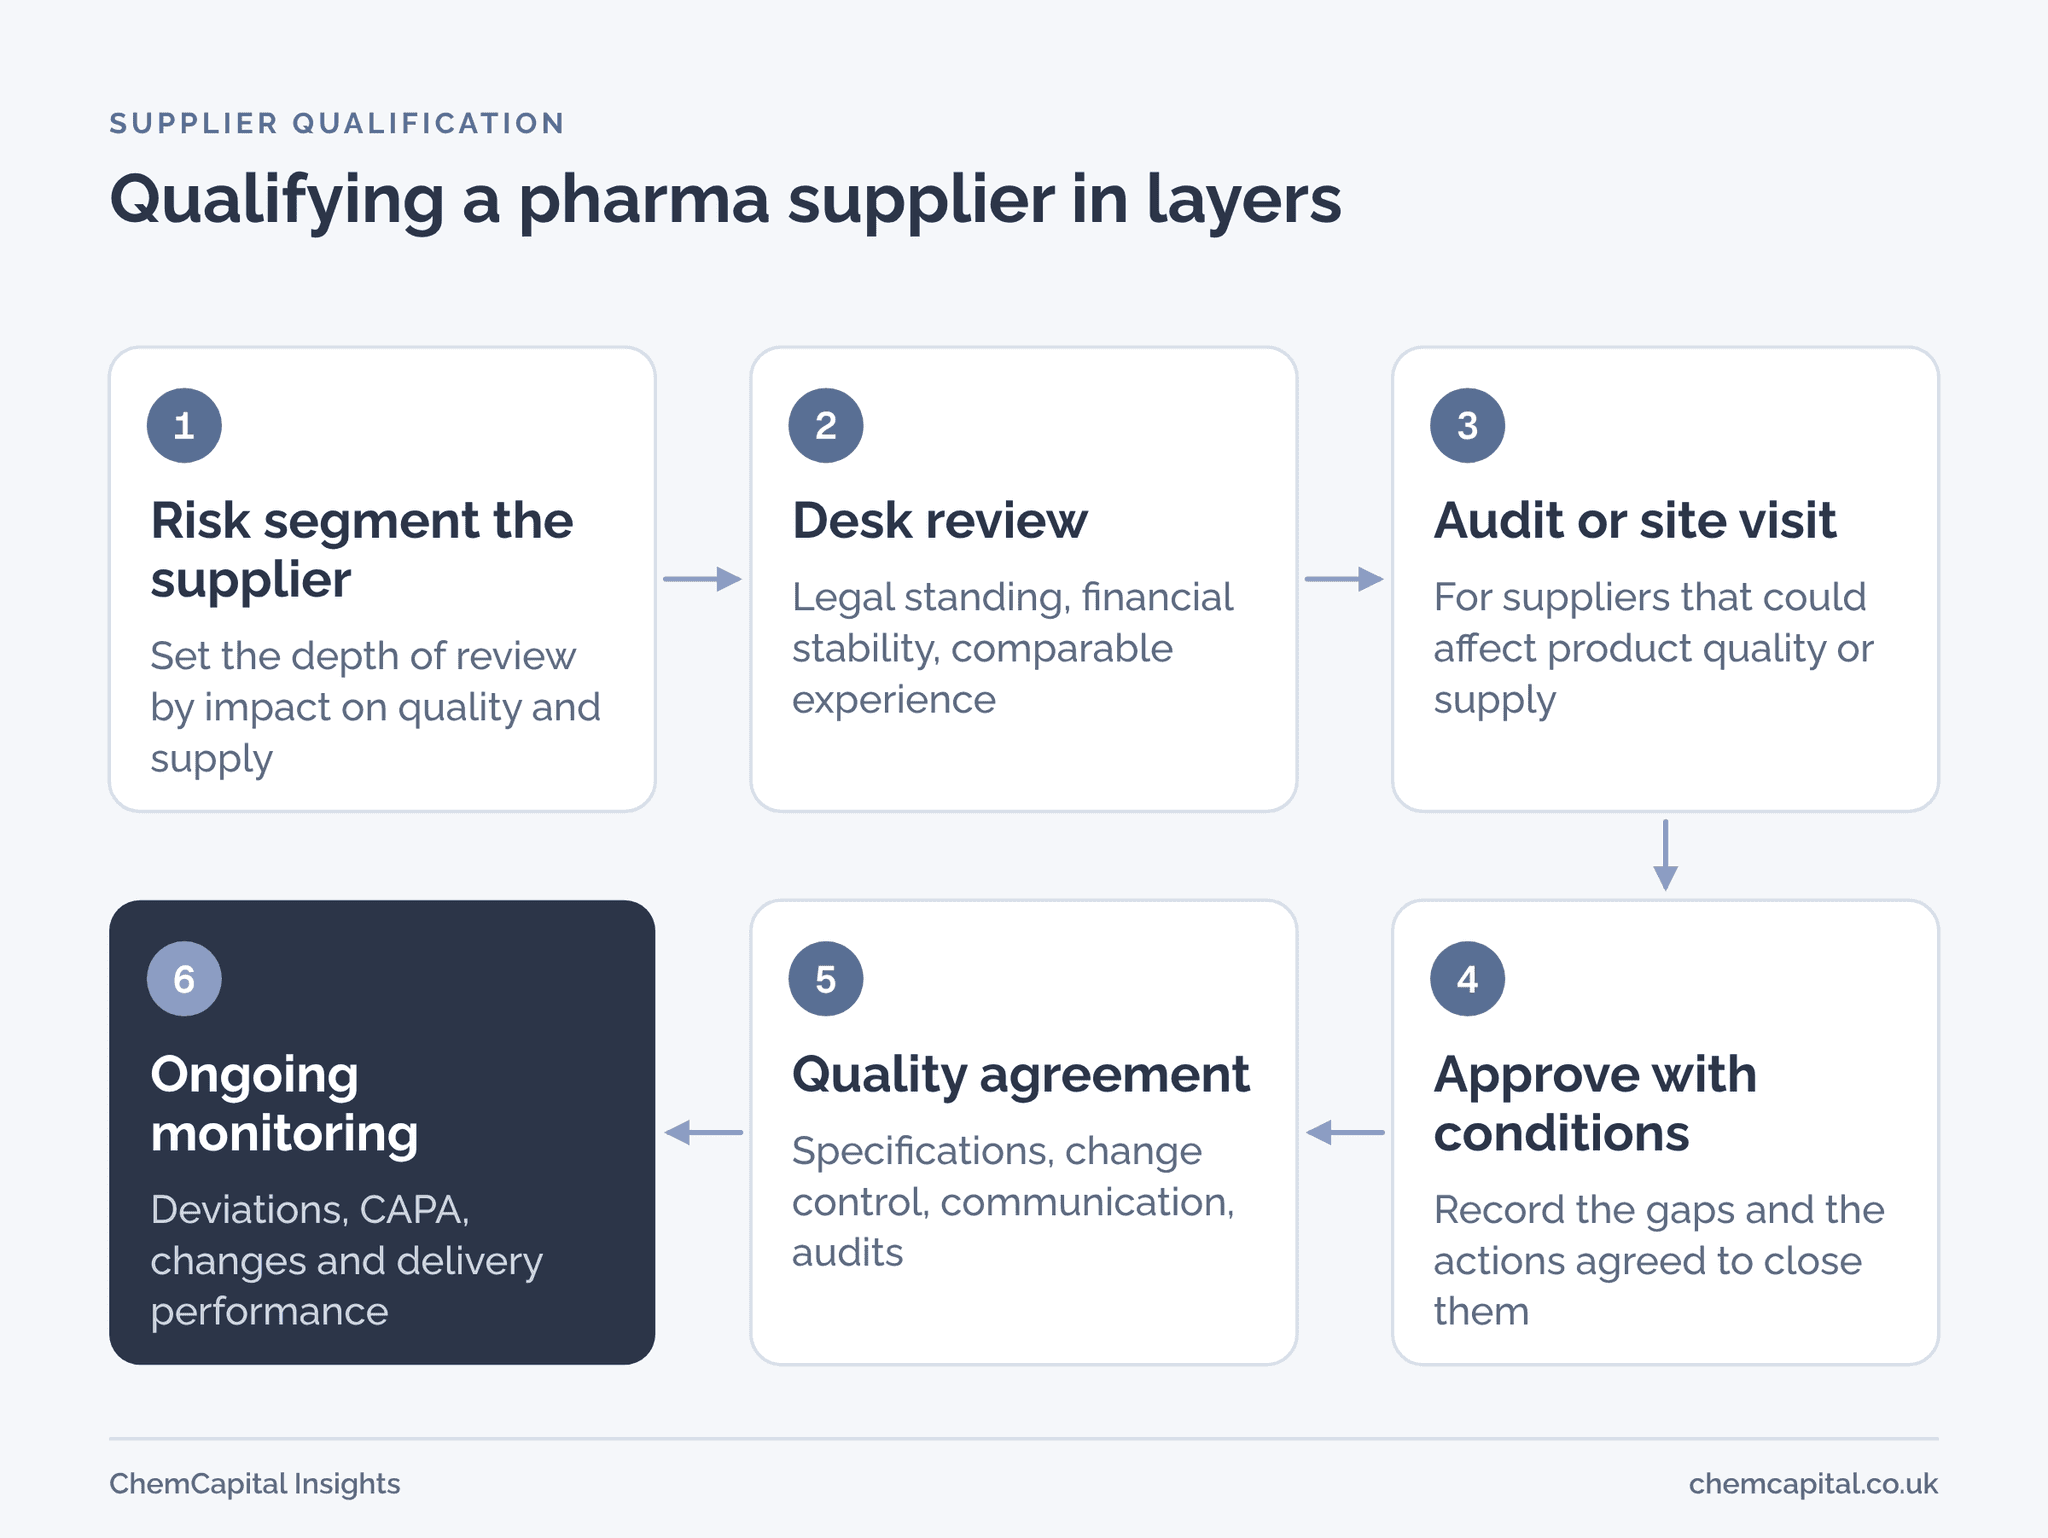
In practice, the strongest teams qualify suppliers in layers. They first check whether the supplier is even eligible to do the work. Then they test whether the supplier is suitable for this specific material, service, or manufacturing context. Then they document responsibilities, communication, and monitoring before award, not after something goes wrong.
Create and manage RFQs in minutes
ChemCapital handles the entire procurement cycle, from structured RFQs and supplier comparisons to formal purchase orders and delivery tracking.
Start with eligibility and legal standing
Before you get impressed by a presentation deck, confirm the basics.
Is the supplier a legally established entity with the right registrations and ownership transparency?
Are there sanctions, debarment, or serious enforcement issues that should stop the process?
Can the supplier show financial stability that fits the length and criticality of the contract?
If the answer is unclear, pause. Qualification gets stronger when procurement filters out obvious noise early and spends its time on suppliers that could realistically become approved sources.
Test relevant experience, not generic capability
A supplier may be excellent in one context and unsuitable in another. The right question is not "Are you capable?" It is "Have you successfully delivered this type of regulated scope under comparable conditions?"
Ask for evidence from comparable contracts, product types, validation expectations, and delivery environments. For higher risk suppliers, a desk review alone is rarely enough. Site visits, audits, or third party appraisals become more important when the supplied material or service could affect product quality, patient safety, compliance, or continuity of supply.[4, 5]
Make quality and ESHS evidence visible
This is where too many qualification processes get vague. For pharmaceutical procurement, quality evidence should be explicit and reviewable.
That may include relevant GMP experience, change control discipline, deviation handling, CAPA maturity, traceability, supplier management, data integrity, and documentation practices. Where outsourced activities are involved, responsibilities and communication processes for quality related work should be written down and monitored. FDA guidance also makes clear that quality agreements should define materials or services, quality specifications, communication mechanisms, change responsibilities, and audit expectations.[1, 2, 3]
Environment, safety, health, and sustainability expectations should also be visible where they are relevant to the scope. The point is not to build a bigger questionnaire. The point is to give the decision team evidence it can defend.
Practical example
A biotech buyer needs a custom skid package for a new manufacturing line. Two suppliers are commercially close.
One supplier looks cheaper on headline price but gives weak answers on validation support, quality escalation, and change control. The other supplier provides stronger evidence, clearer responsibilities, and better documentation discipline.
In a weak process, procurement picks the cheaper number and uncovers the risk later.
In a strong process, qualification recognises validation delay as a real commercial cost, not just a QA inconvenience, and the team can justify the stronger supplier choice before award.
Bring supplier evidence into the decision
If your qualification process still lives across email attachments, spreadsheet tabs, and disconnected audit notes, you are adding risk without meaning to. ChemCapital helps teams structure supplier evidence, connect qualification to RFQ decisions, and keep sourcing logic visible from scope through award. See how ChemCapital works or explore benefits for procurement teams.
Ready to put supplier evidence at the centre of your next award? Start a free 14 day ChemCapital trial, with no credit card needed, and run your next qualification and RFQ in one place.
Continue reading
Informational only, not procurement or legal advice. Cited names, frameworks, and statistics belong to their respective owners.
Create and manage RFQs in minutes
ChemCapital handles the entire procurement cycle, from structured RFQs and supplier comparisons to formal purchase orders and delivery tracking.
Start for freeRelated articles
Design Qualification (DQ) for GMP Equipment: What It Is and What the Vendor Provides
Design qualification is the documented check that a proposed equipment design meets the URS and GMP before it is built. Here is where DQ sits in EU GMP Annex 15, what evidence the vendor supplies, and a DQ checklist.
Requirements Traceability Matrix for GMP Equipment: From URS to PQ
A requirements traceability matrix links every URS line to the design document that meets it and the test that proves it, from DQ through FAT, SAT, IQ, OQ and PQ. Here is how to build one, with a template.
How to Prepare for a Customer Quality Audit as an Equipment Manufacturer
A practical guide for equipment makers facing a customer or vendor audit: the documents to have ready, how to run the walk through, the findings auditors raise most often and how to close them properly.